How Do You Qualify Direct Thermal Labels for Automated Parcel Sortation
Automated sortation exposes labels to high-speed conveyors, variable package orientation, scanners, and repeated mechanical contact. A label qualifies only when it feeds reliably in the printer, adheres after application, and scans through the complete line. Bench scans and a few hand-labeled cartons are useful screening but not enough for approval.
When comparing sortation barcode labels, match the material to the actual surface, printer, handling time, and scan conditions. A familiar size or low roll price does not prove the label will work in the complete workflow.
What the Label Must Accomplish
Map the line’s barcode readers, camera angles, lighting, package speeds, and acceptable label placements. Identify the carrier or internal barcode that actually drives routing. A code placed on a curved parcel or near a tape seam may be read inconsistently even when the bars themselves are sharp. Decide whether both human-readable tracking text and barcode must survive a chute or accumulation area. Material selection follows these process requirements.
Choosing the Label Construction
Choose facestock, topcoat, and adhesive for abrasion, package surfaces, dwell time, and any moisture exposure. Specify roll dimensions and die-cut consistency so high-speed printers and applicators feed without drift. If different package materials share the line, qualify the stock on each major substrate. A label that passes on new corrugated board may fail on glossy mailers or heavily recycled cartons. Consider separate constructions only when one stock cannot meet the full mix.
Printing and Barcode Setup
Use the official barcode layout and do not scale it to fill a smaller stock. Leave quiet zones clear and align print darkness with the selected paper. Verify the output at the fastest printer setting planned for production. Include the first label after a roll change and the last labels on a roll in the trial. A barcode verifier can help diagnose print quality, but the line’s actual scanner is the final test for the specific conveyor environment.
Application in the Real Workflow
If labels are applied automatically, check web tension, peel position, tamp pressure, and package detection. If applied manually, standardize the permitted carton faces and train staff to avoid seams and tape. Confirm sufficient dwell before the parcel enters a fast belt, particularly on dusty or cold surfaces. A lifted leading edge can be caught by a guide and turn an adhesion problem into a jam that affects the whole line.
A Test That Reveals Problems Early
Run representative parcels through every normal route at production speed. Include smallest and largest packages, rigid cartons, flexible mailers, and the known difficult surface. Record no-read rate, misroutes, rejected labels, print errors, and physical damage. Repeat after a roll change and a printer restart. Use enough parcels to reveal intermittent failures and keep the failed units for root-cause review, rather than reporting only an average pass rate.
Common Failures and Their Causes
A no-read may come from barcode design, poor print, bad placement, scuffing, or a scanner setting. Investigate the physical label before changing material. If unreadable parcels cluster on one package type, examine substrate and geometry. If errors grow after a roll change, inspect setup and die-cut pitch. A single supplier claim about ‘high-speed compatibility’ does not replace measured line performance under the site’s conditions.
What to Request From a Supplier
Provide the supplier with printer and applicator models, stock dimensions, package mix, line speed, scan equipment, label position, and environmental exposure. Define an acceptable no-read rate and what constitutes a material-related failure. Request samples from normal production converting, then run a witnessed site trial. Keep the exact construction and roll specification fixed after approval unless a change passes the same qualification route.
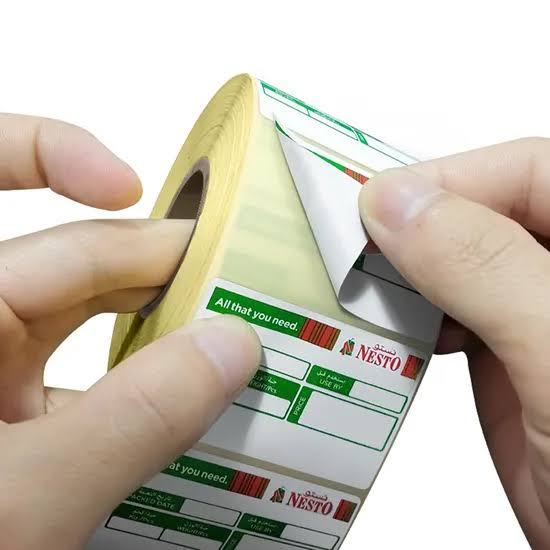
To order direct thermal parcel labels for this sortation barcode labels use case, specify the target surface, label life, printer model, size, core, winding, adhesive, and expected handling. Ask for a converted-roll sample in the proposed construction. The sample should pass the field test outlined above before the full purchase.
How to Separate Label and Line Problems
Collect failed parcels rather than discarding them immediately. Compare a failed label with a successful one from the same roll and printer. Check barcode quality before the parcel enters the line, then inspect after the point where no-reads rise. If good labels fail only at one camera, the issue may be lighting, alignment, or software. If failures follow one package surface, investigate adhesive and placement. This disciplined comparison prevents a stock change from masking an equipment fault or vice versa.
What a Material Change Should Trigger
A new facestock, adhesive, liner, die cut, or roll winding can affect a high-speed line even when the printed label looks unchanged. Require change notification from the converter and rerun relevant printer, applicator, and sortation checks before switching stock. Keep retained rolls from the approved batch for comparison. For multi-site operations, release the change one site at a time with recorded scan results. A controlled transition is cheaper than discovering at peak volume that a substitute stock causes intermittent no-reads.
Ask the sortation team to preserve a small set of failures from each trial, including the package and the exact location of the label. A spreadsheet of no-read counts cannot show whether the barcode was creased, scuffed, partly covered, or printed too close to an edge. Physical examples make the next corrective action more precise.
How to Decide Whether the Trial Passed
Set the acceptance criteria before testing sortation barcode labels. Record feed errors, print clarity, barcode scan rate, application time, edge lift, removal or residue where relevant, and damage after ordinary handling. Use the hardest surface and longest planned dwell period, not only a fresh label under ideal office conditions. If a sample fails, change one factor at a time so the result identifies whether print setup, facestock, adhesive, label geometry, or application method is responsible. Keep the approved sample and settings with the purchasing specification.
Does a Barcode That Scans by Hand Qualify for Sortation
No. A handheld reader can be moved closer or angled until it succeeds. Automated equipment reads at fixed positions and speed. Qualify the label on the installed line, including normal package variation and post-handling condition.